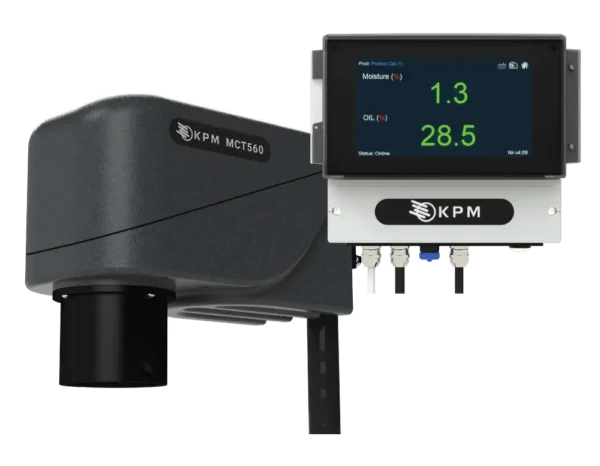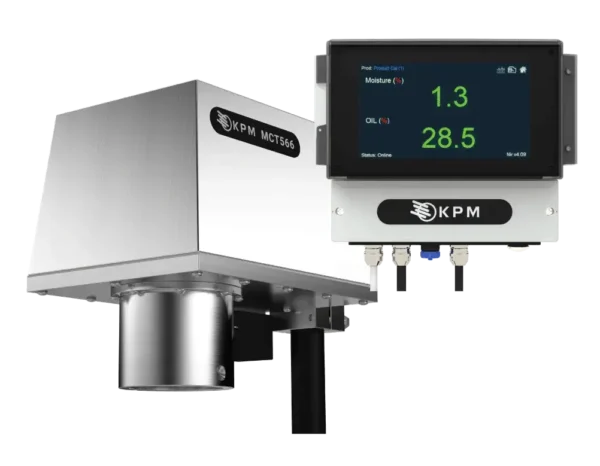
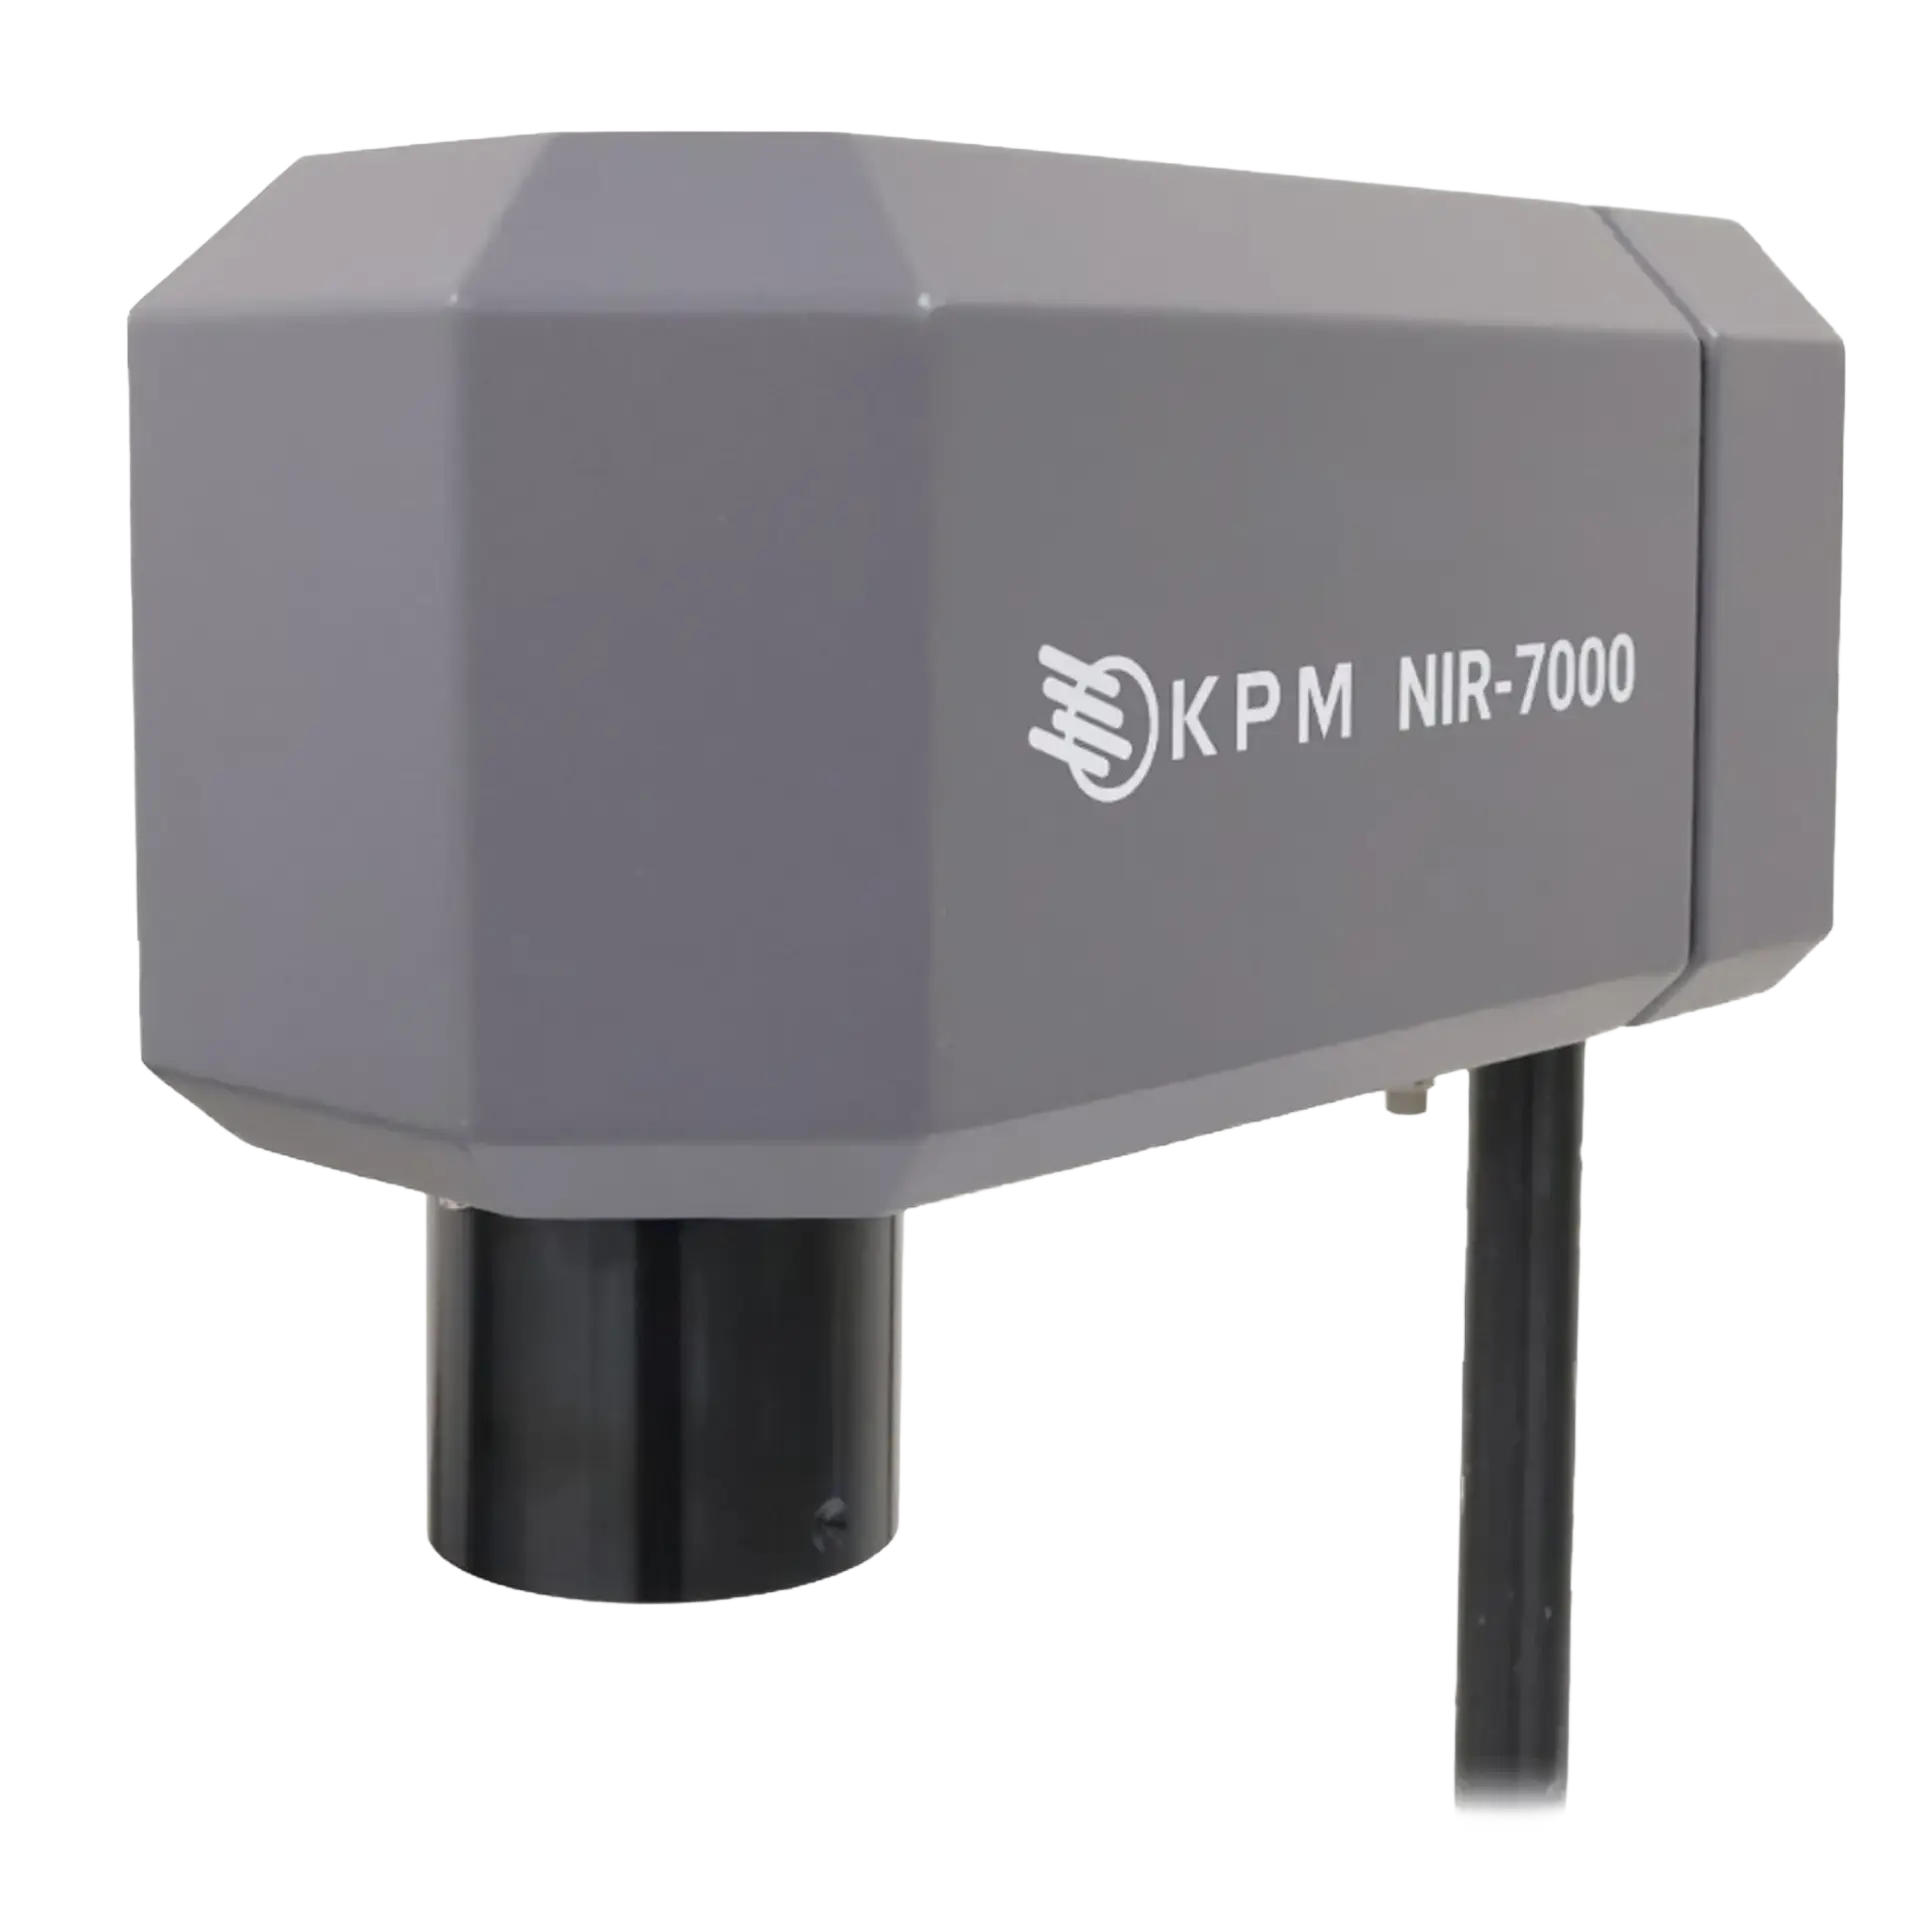
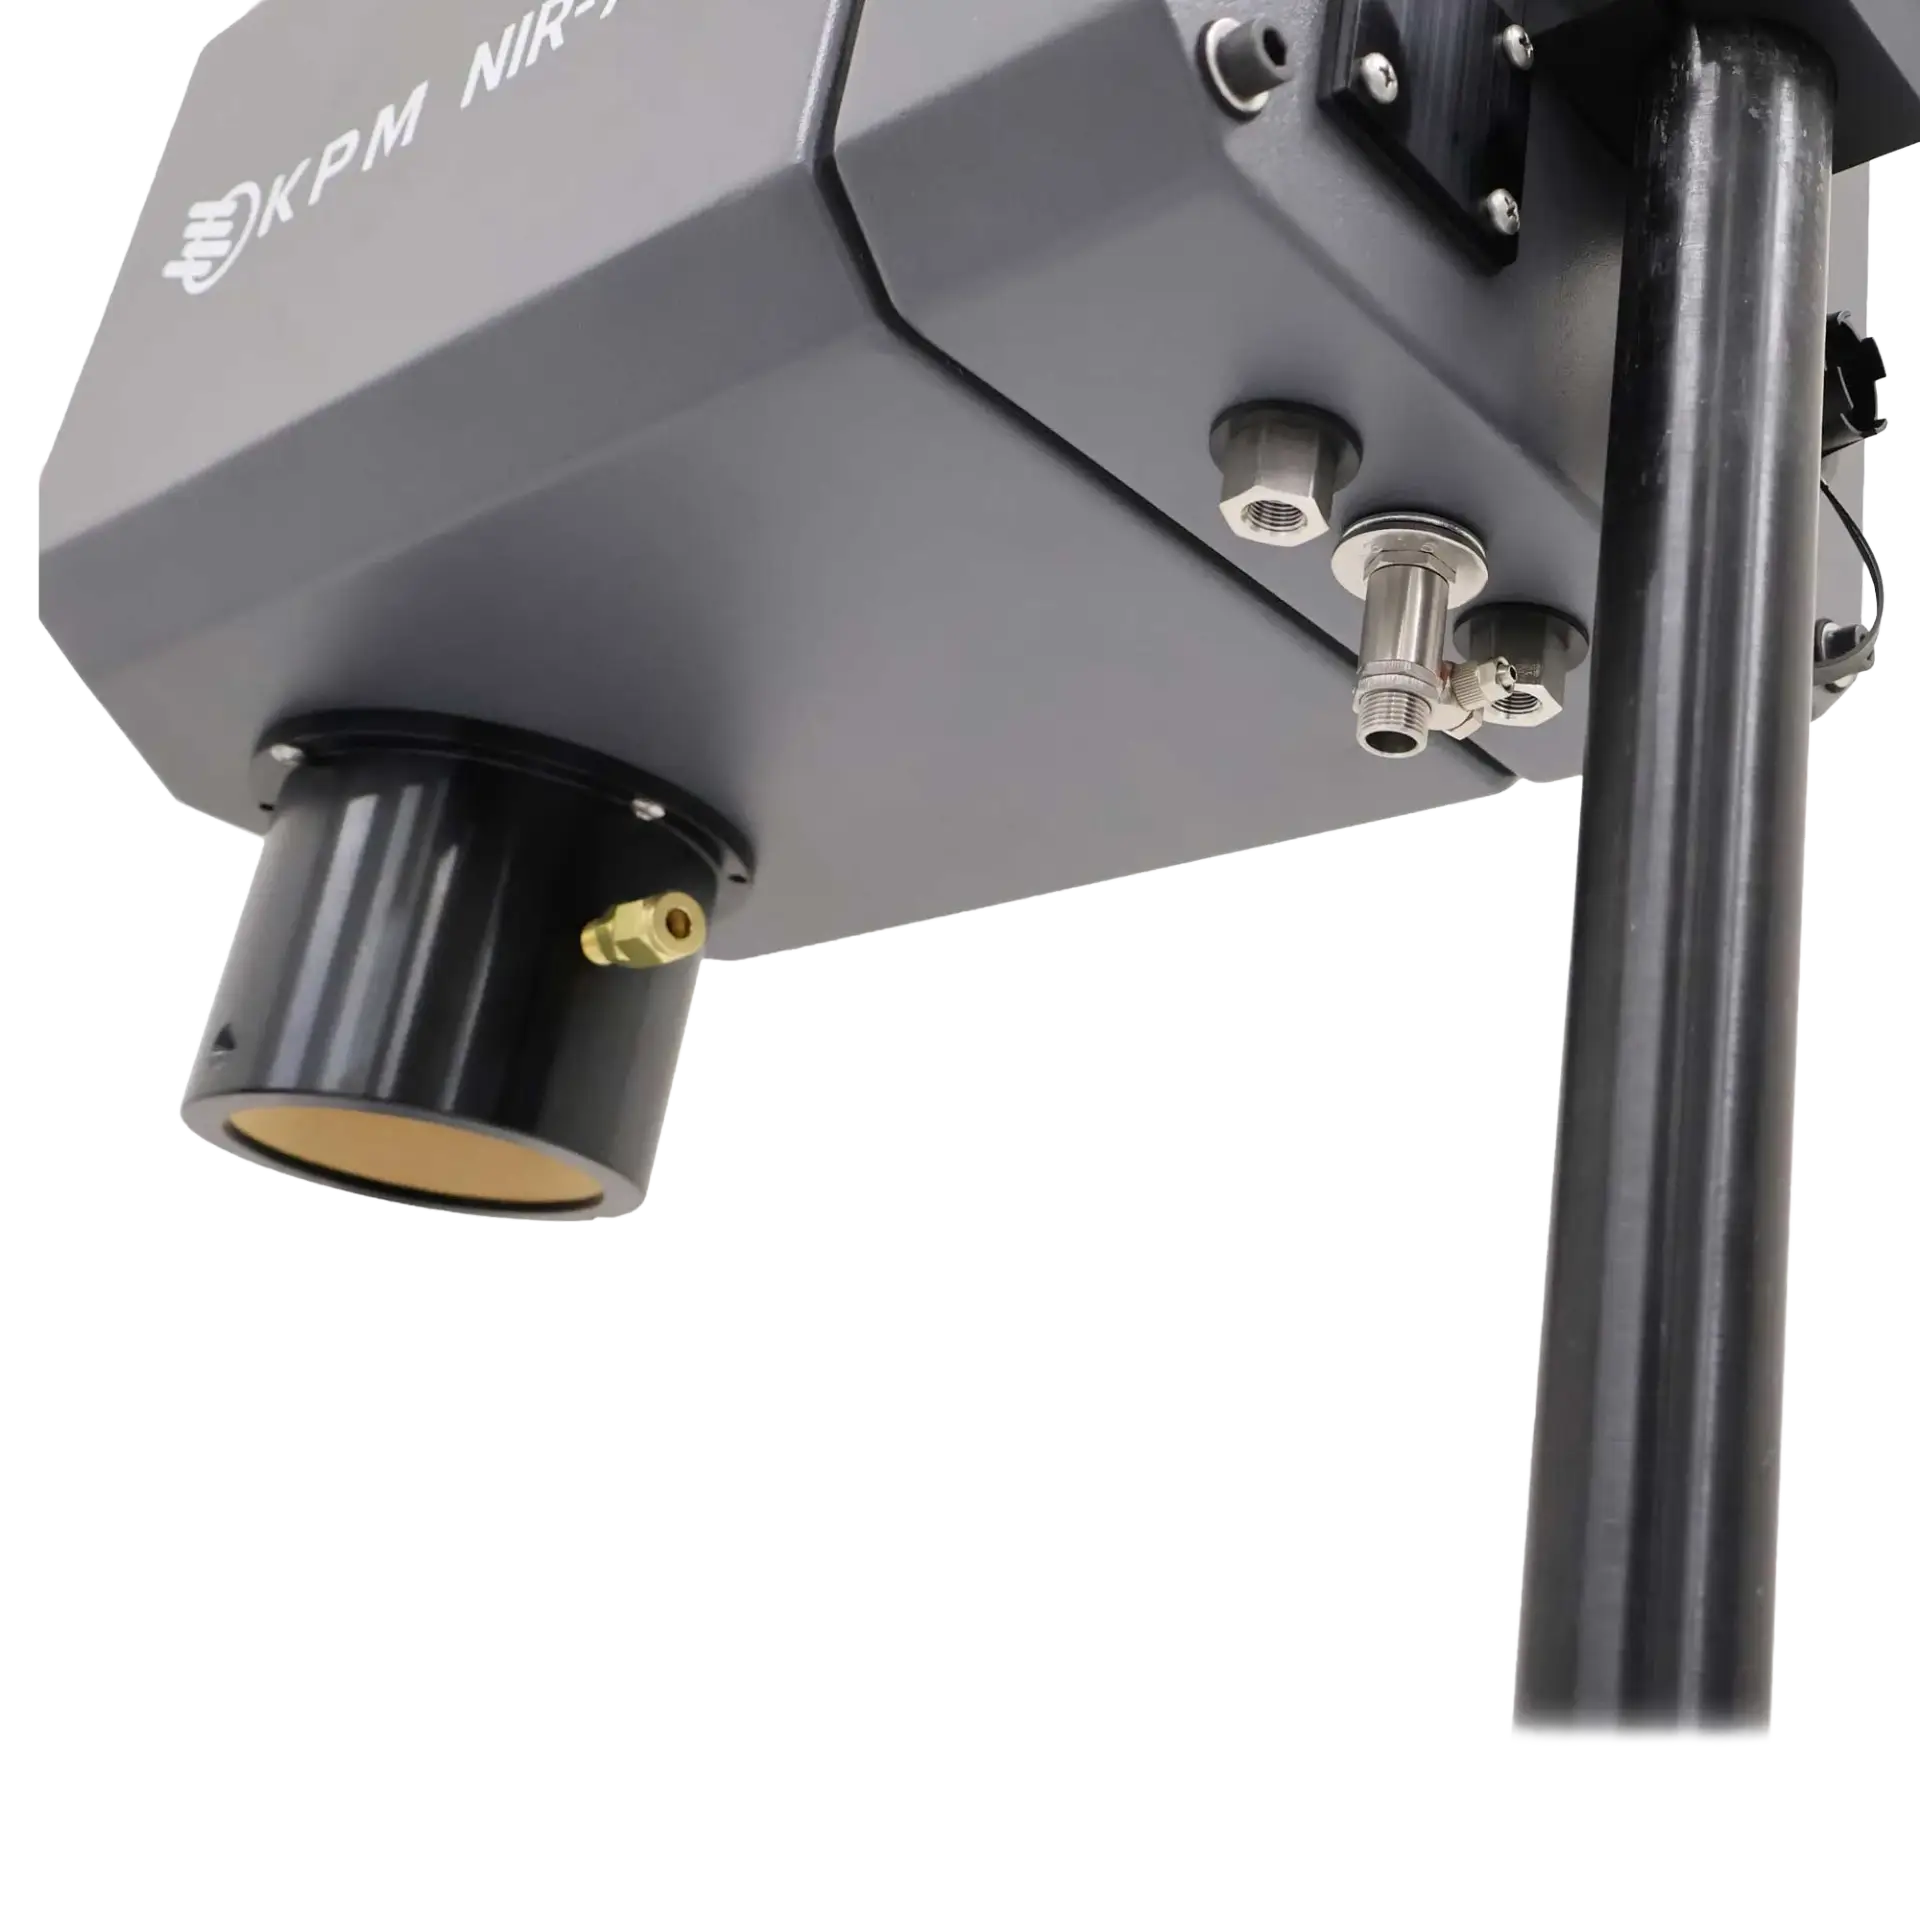
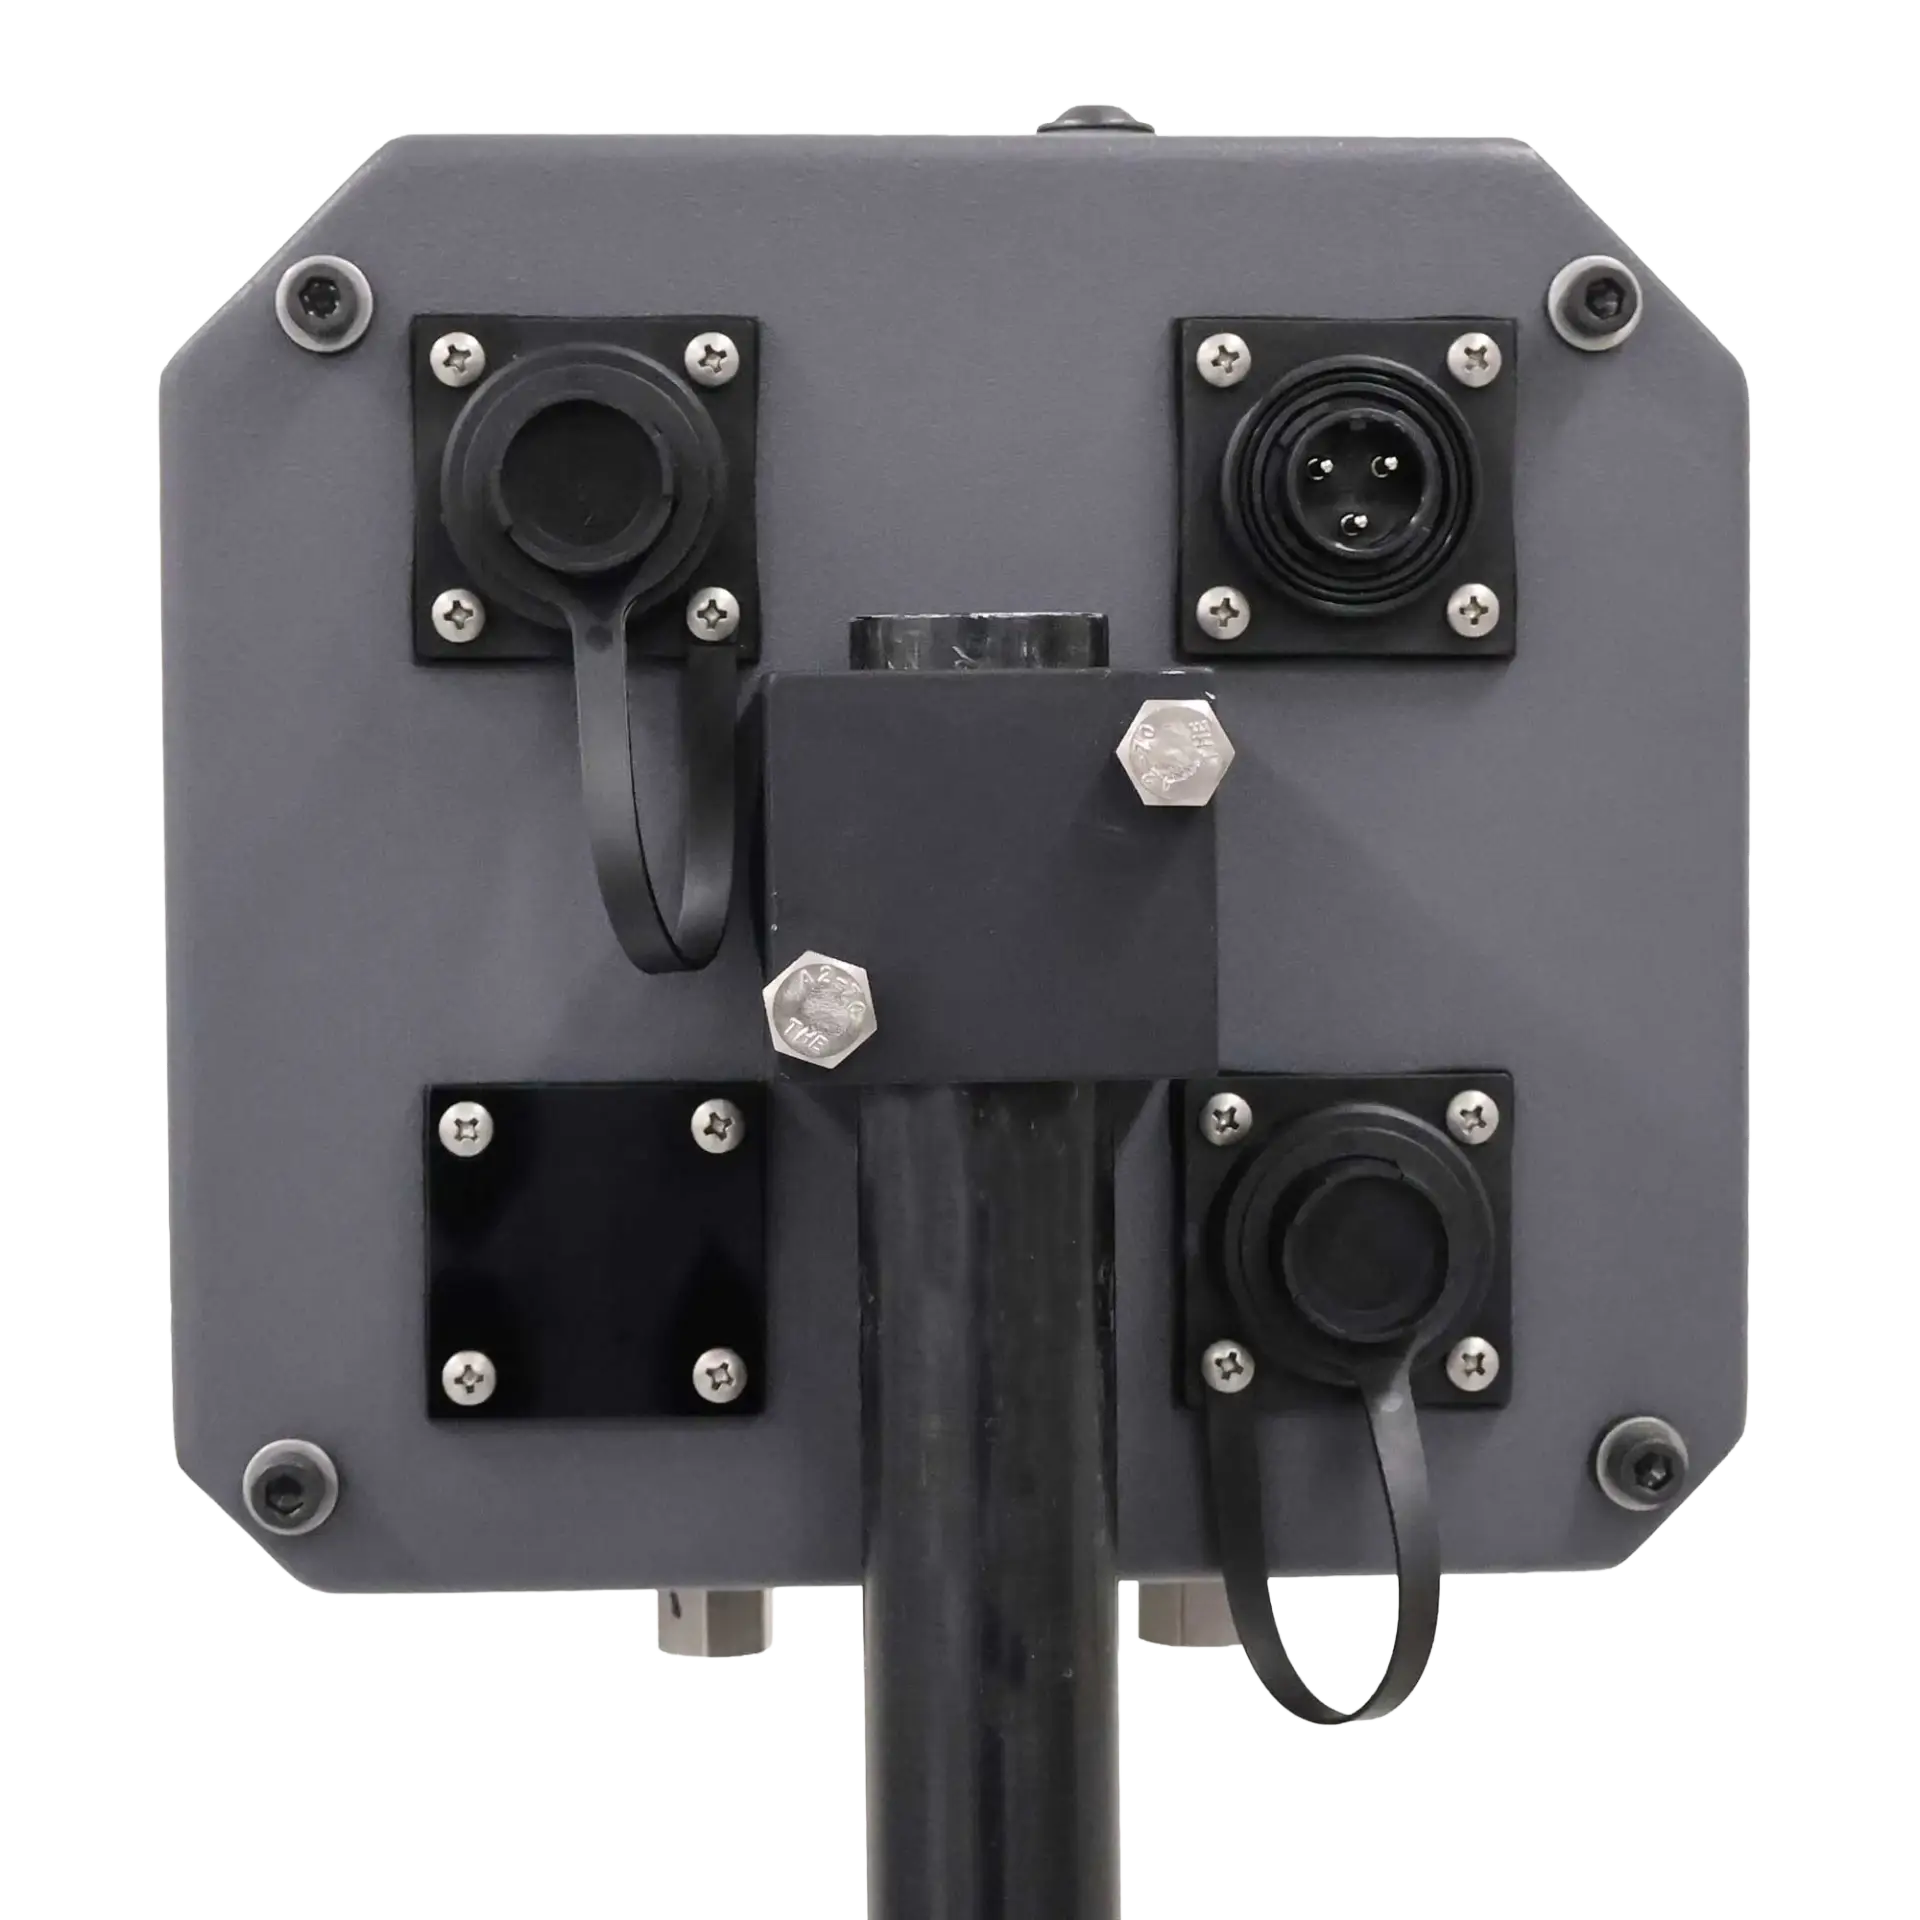
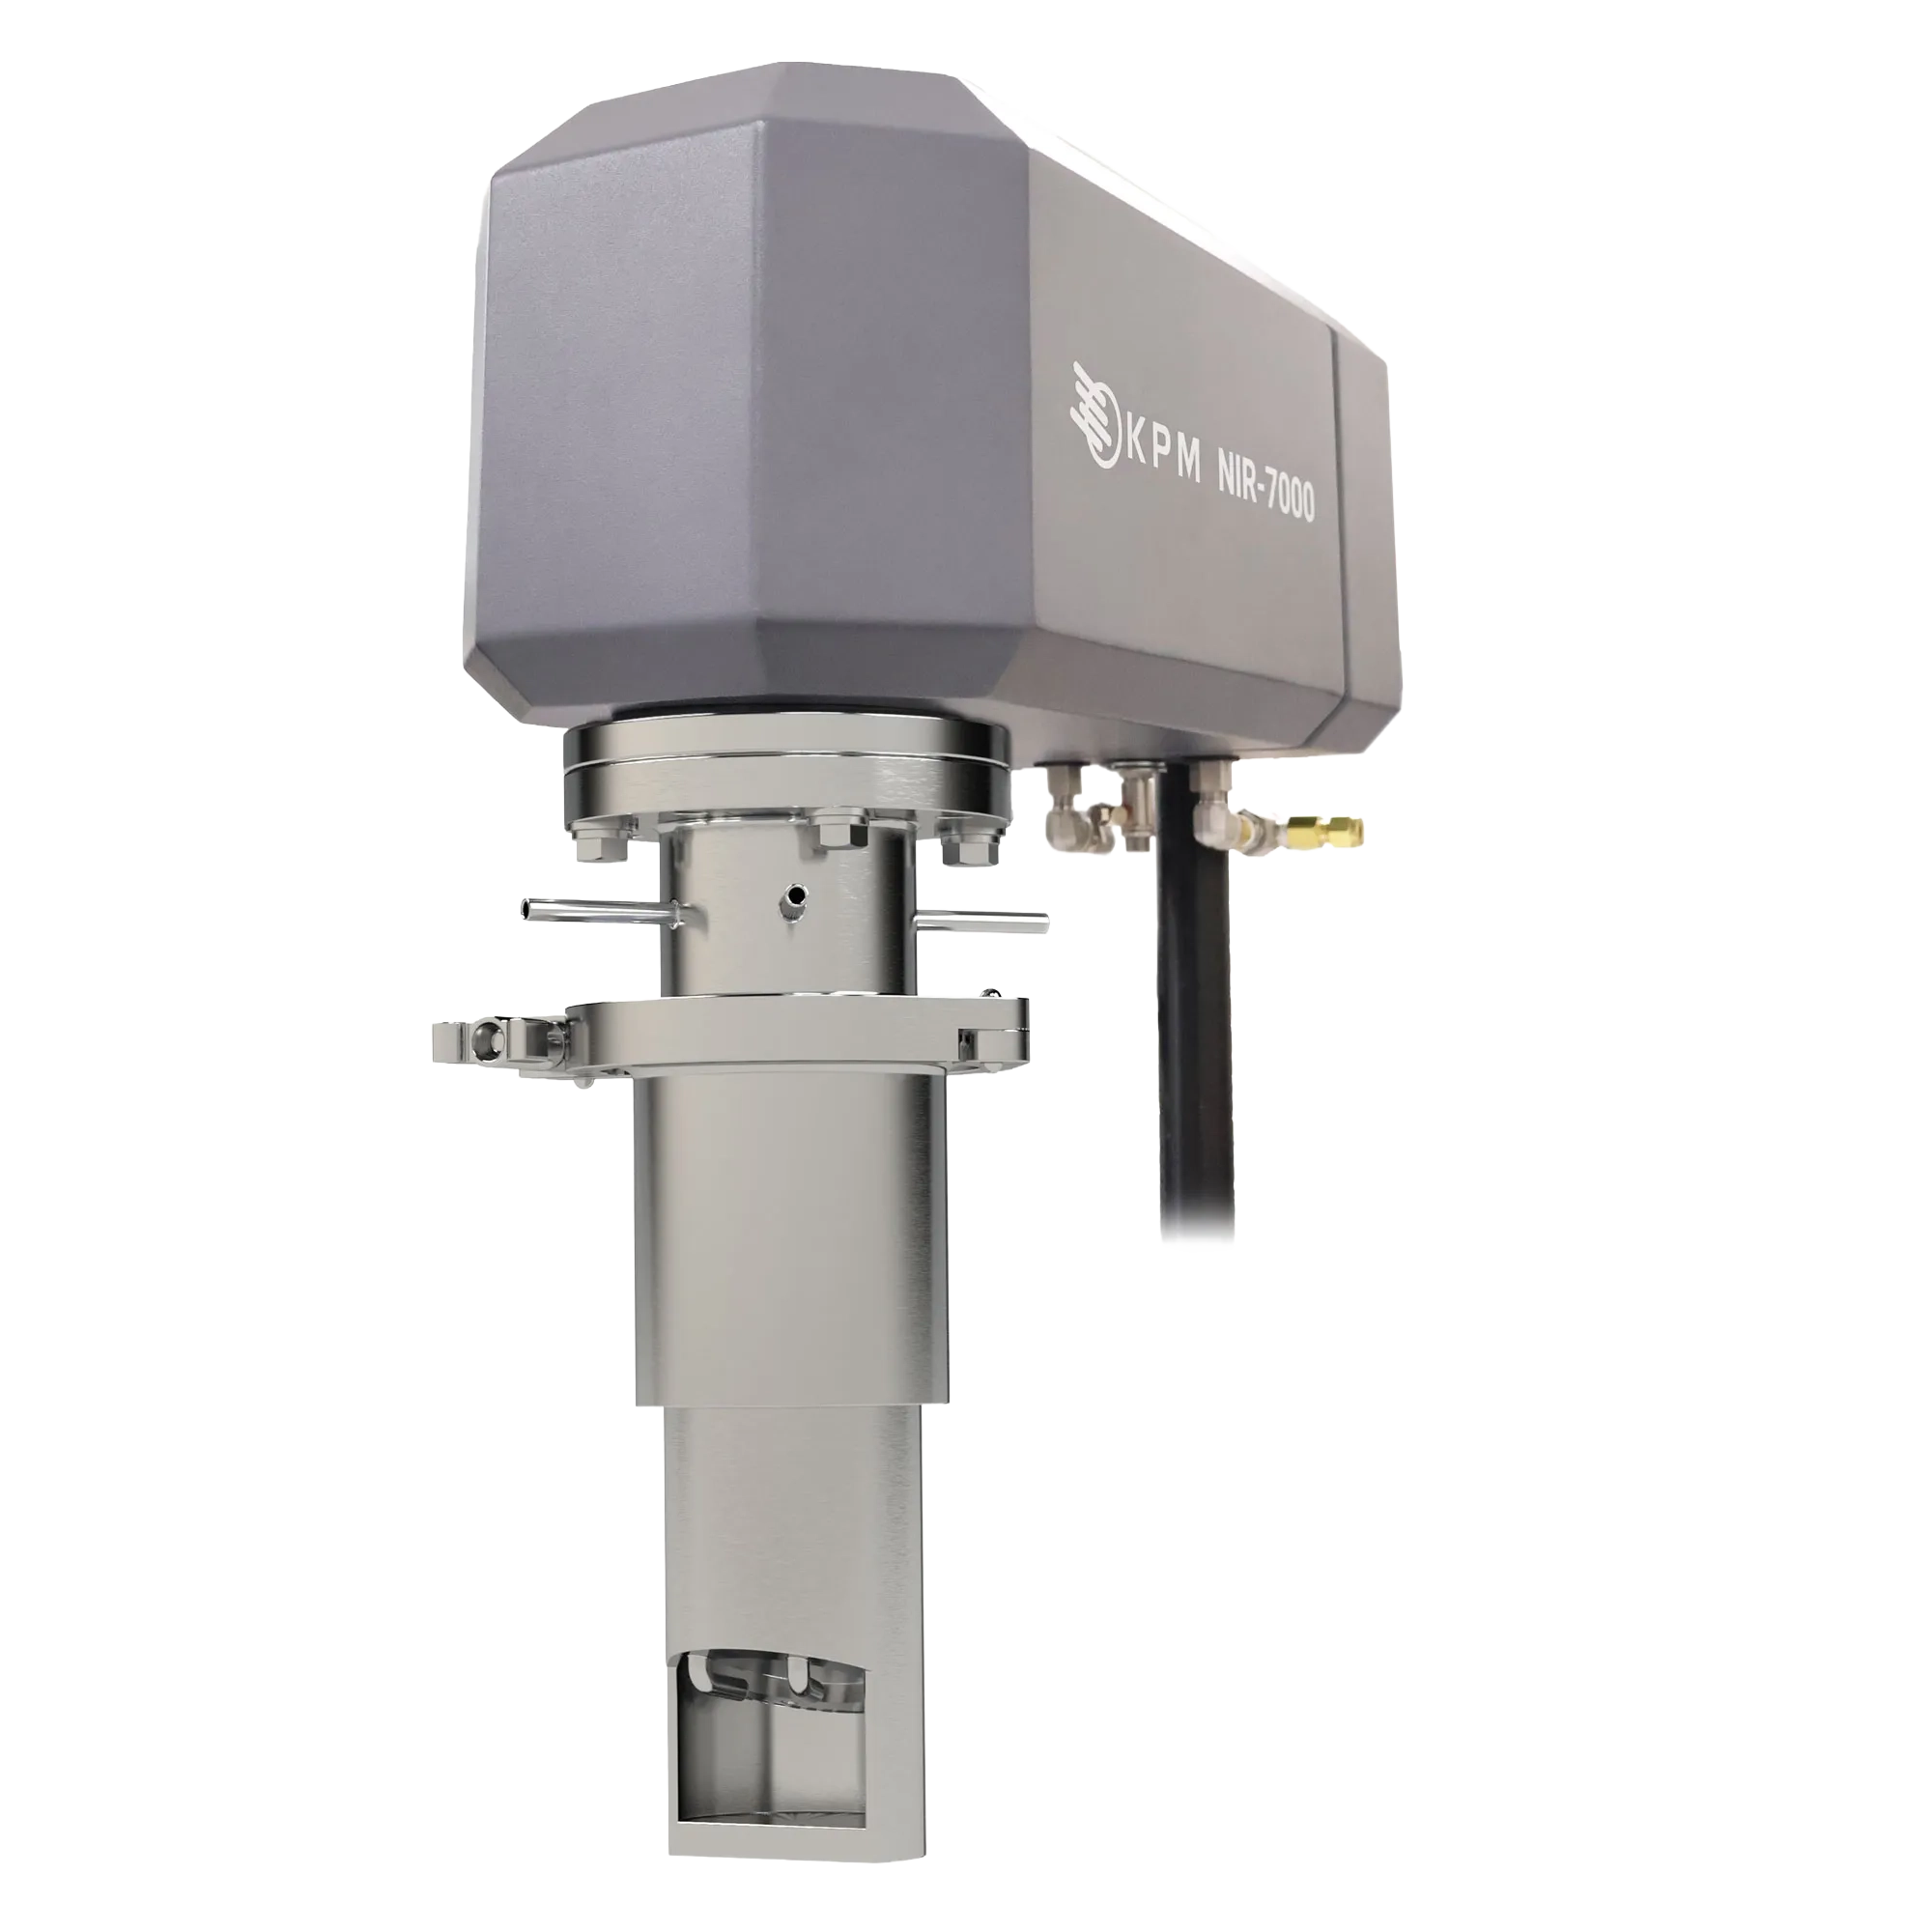
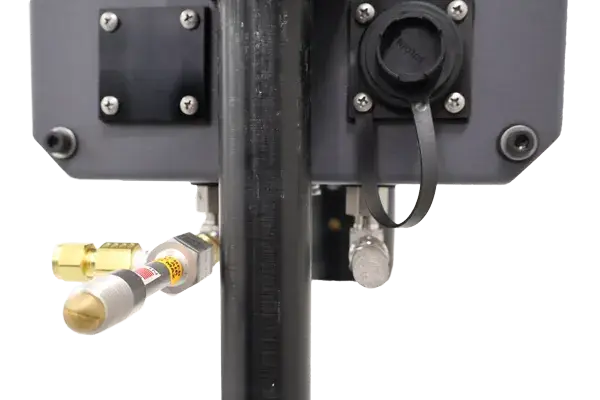
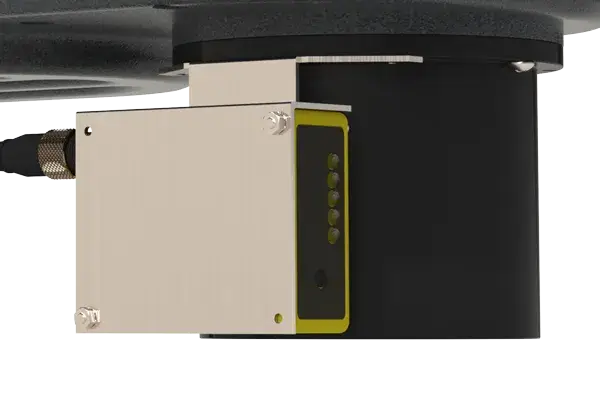
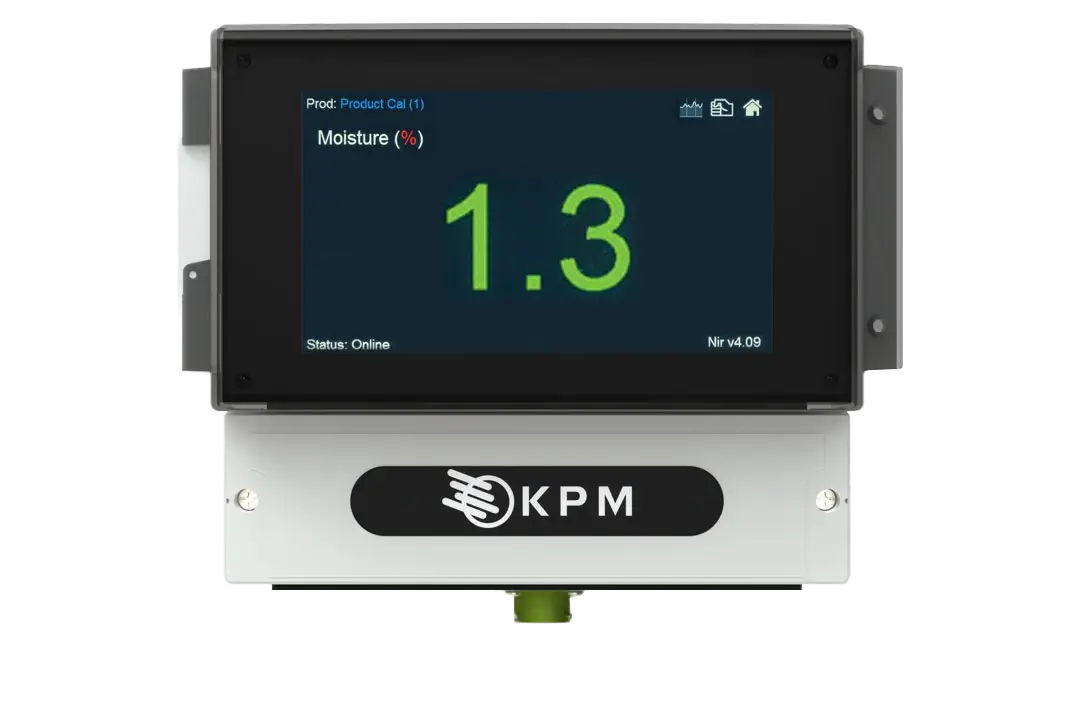
The NIR-7000 is a next-generation online NIR moisture sensor engineered for continuous, non-contact moisture measurement in demanding industrial environments. Delivering accuracy to within ±0.10%, this IP65-rated analyser suits wood products, building materials, pulp & paper, minerals and textile manufacturing lines that need real-time process control, reduced energy costs and improved product quality.
The NIR-7000 is a continuous in-line near-infrared (NIR) analyser that delivers reliable, non-contact moisture measurements directly in your process environment for real-time monitoring and control of almost any production line. As the next-generation replacement for the widely used Sensortech NIR-6000, the NIR-7000 features an updated optical platform built for high-throughput industrial applications — including wood, building materials, pulp & paper, minerals, textiles and chemicals — where moisture content directly impacts product quality.
Capturing measurements every four milliseconds, the NIR-7000 automatically adjusts your process to hit moisture targets, cut energy costs and protect your bottom line.
A halogen light source shines through a rotating filter wheel spinning at 2,000 RPM, isolating the specific NIR wavelengths relevant to moisture. The reflected light is focused onto a cooled sulfide detector, and the on-board smart circuit board compares the signal to an internal reference beam, converting it into a precise moisture percentage — continuously, in real time.
The NIR-7000 can be delivered pre-calibrated for a wide range of products conveyed on a belt, through an auger, or viewed through a sight-glass window in a bin or chute, including:
Every NIR-7000 ships with a powder-coated sheet metal IP65 housing, advanced digital noise filtering hardware, pre-programmed algorithms and calibrations, specialised NIR filtering to suit your application, SensorVu management software, and power and connection cables. Backed by a two-year factory warranty on parts and labour, with a three-year warranty on the lamp.
Talk to the Techotrix team to find out whether the NIR-7000 is the right fit for your production line.
| Dimensions (W x D x H) | 215.9 mm x 447.0 mm x 281.9 mm (8.5 in x 17.6 in x 11.1 in) |
| Weight | 9.5 kg (21 lbs) |
| Power | 100–240 VAC (50/60 Hz), 42W; 24VDC upon request |
| Sensor Housing | Powder-coated sheet metal |
| Moisture Accuracy | ± 0.10% (subject to application) |
| Moisture Range | 0 to 95% |
| Recommended Measurement Distance | 200–450 mm (8–18 in) |
| Calibration Codes | 100 |
| Ambient Temperature | 0 to 55°C (32 to 131°F), up to 85°C (185°F) with cooling option |
| Standard Mount | Top or rear mount for positioning over conveyor belts, augers/screw conveyors, or looking through a sight glass window |
| IP Rating | IP65 |
| Interfaces | Standard: Ethernet TCP/IP, isolated 4-20mA outputs Optional: EtherNet/IP, EtherCAT, ProfiNet, ProfiBus, Modbus TCP, DeviceNet, OPC-DDE Server |
| Warranty | Two years parts & labour; three years on lamp replacement |
The NIR-7000 can be configured with the following accessories and interface options to suit your installation:
Communication interfaces: Standard Ethernet TCP/IP and isolated 4-20mA outputs, with optional EtherNet/IP, EtherCAT, ProfiNet, ProfiBus, Modbus TCP, DeviceNet or OPC-DDE Server for integration into existing PLC/MES systems.
Power option: Standard 100–240 VAC, or 24VDC available upon request.