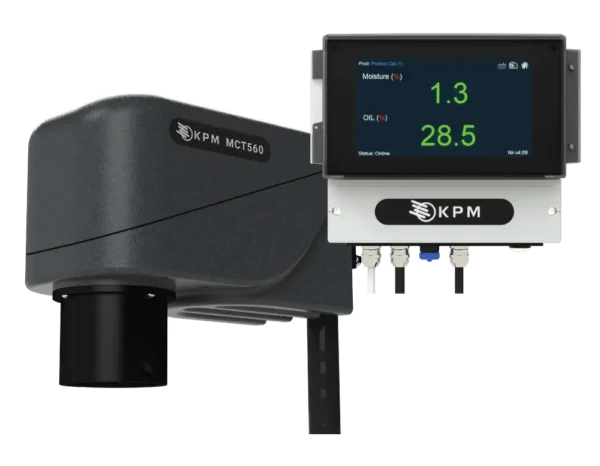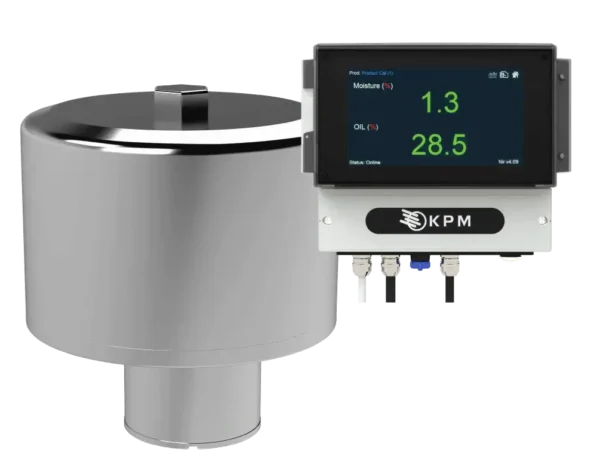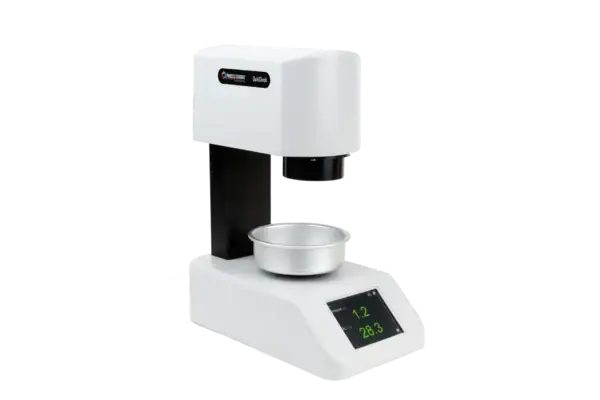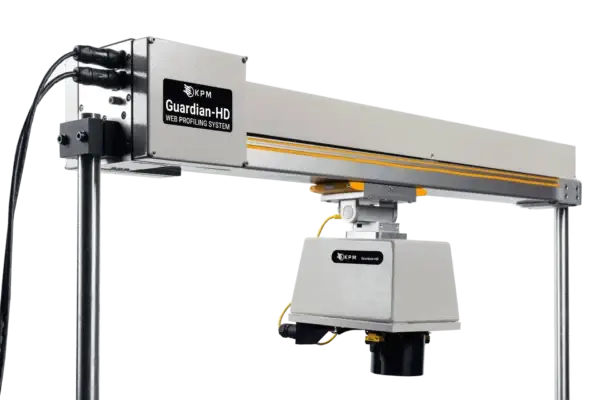


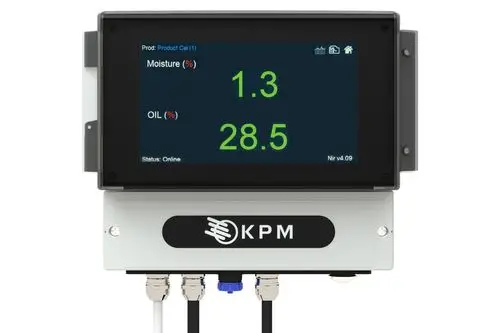


The MCT460 is a proven industrial online NIR sensor for continuous, non-contact measurement of moisture, oil/fat, coat weight and product temperature. Accurate to within ±0.1% moisture, it’s a rugged, field-serviceable analyser trusted across paper, wood, fertiliser, tobacco and converting applications.
MCT460 online sensors help operators control moisture within one-tenth of a percent to meet product specifications every time. The MCT460 features NIR technology widely used and accepted across industries for moisture and other online measurements.
Light from the lamp is directed through a rotating filter wheel spinning at 2,000 RPM, isolating the NIR wavelengths relevant to your application. The reflected light is captured by a mirror and focused onto a Peltier-cooled lead sulfide detector. The on-board smart circuit board compares this to an internal reference beam, converting it into a precise percentage of moisture, oil or other parameters — continuously, in real time.
The MCT460 continuously measures and controls moisture, coat weight, film thickness and product temperature during manufacturing, and can drive closed-loop control of belt speed, paper re-moisturisers and other moisture-critical processes. Typical applications include fertilisers, paper products, wood products, converting (hot melts, pressure sensitive adhesives) and tobacco, with additional applications across extruded plastics, PVB film, textiles, crumb rubber, PVC powders, ceramics, detergents and soaps, ore, and biofuels.
The MCT460 ships in an industrial-grade cast aluminium or electroless-nickel enclosure with a local display and all power, digital and analogue inputs built in for straightforward installation. It mounts 200–450 mm (8–18 in) above belt conveyors for continuous product flow, offset to the side of the shaft on augers and screw conveyors, or through a sight glass window on bins and chutes — with an optional snorkel sampler for free-falling powders and granules.
All MCT Series models run KPM’s proprietary SensorVu Windows-based PC software for set-up, calibration, product code selection, diagnostics and remote trend monitoring across multiple analysers. The MCT460 is backed by a two-year parts and labour warranty, with three years on lamp replacement.
Talk to the Techotrix team to find out whether the MCT460 is the right fit for your production line.
| Sensor Enclosure | Powder-coated cast aluminium |
| Reading Speed | Up to 33 readings/second |
| High-Speed Gating Available? | No |
| Communication Options | USB, Ethernet TCP/IP, EtherNet/IP, EtherCAT, ProfiNet, ProfiBus, Modbus TCP, DeviceNet, OPC-DDE Server |
| Product Calibrations | 100 |
| Measured NIR Constituents | 1, 2 or 3 simultaneously |
| Moisture Accuracy | ± 0.1% |
| Fats/Oil Accuracy | ± 0.2% |
| Wet Basis Moisture Range | Min. 0.1%, Max. 90% |
| Dry Basis Moisture Range | Min. 0.1%, Max. 400% |
| Transmitter/Product Distance | 200–450 mm (8–18 in) |
| Operator Interface | 178 mm (7 in) touch screen |
| Outputs | 4-20mA, 0-10V (isolated) |
| Languages | 13 selectable languages |
| Weight | 8.6 kg (19 lbs) |
| Ambient Temperature | 0–50°C (32–120°F); up to 80°C (160°F) with water or air cooling |
| Power Inputs | 110–240V standard; 24VDC optional |
| Cable | 3 m (10 ft) standard; up to 30 m (100 ft) |
| Compliance | CE Certified (FCC CFR 47: Part 15: B: 2015, Industry Canada ICES-003: 2021) |
| Warranty | Two years parts & labour; three years on lamp replacement |
The MCT460 can be configured with the following accessories and interfaces:
Communication interfaces: USB and Ethernet TCP/IP as standard, with optional EtherNet/IP, EtherCAT, ProfiNet, ProfiBus, Modbus TCP, DeviceNet or OPC-DDE Server for integration into existing PLC/MES systems.
Power option: Standard 110–240V, or 24VDC available as an option. Cable lengths up to 30 m (100 ft) available.